
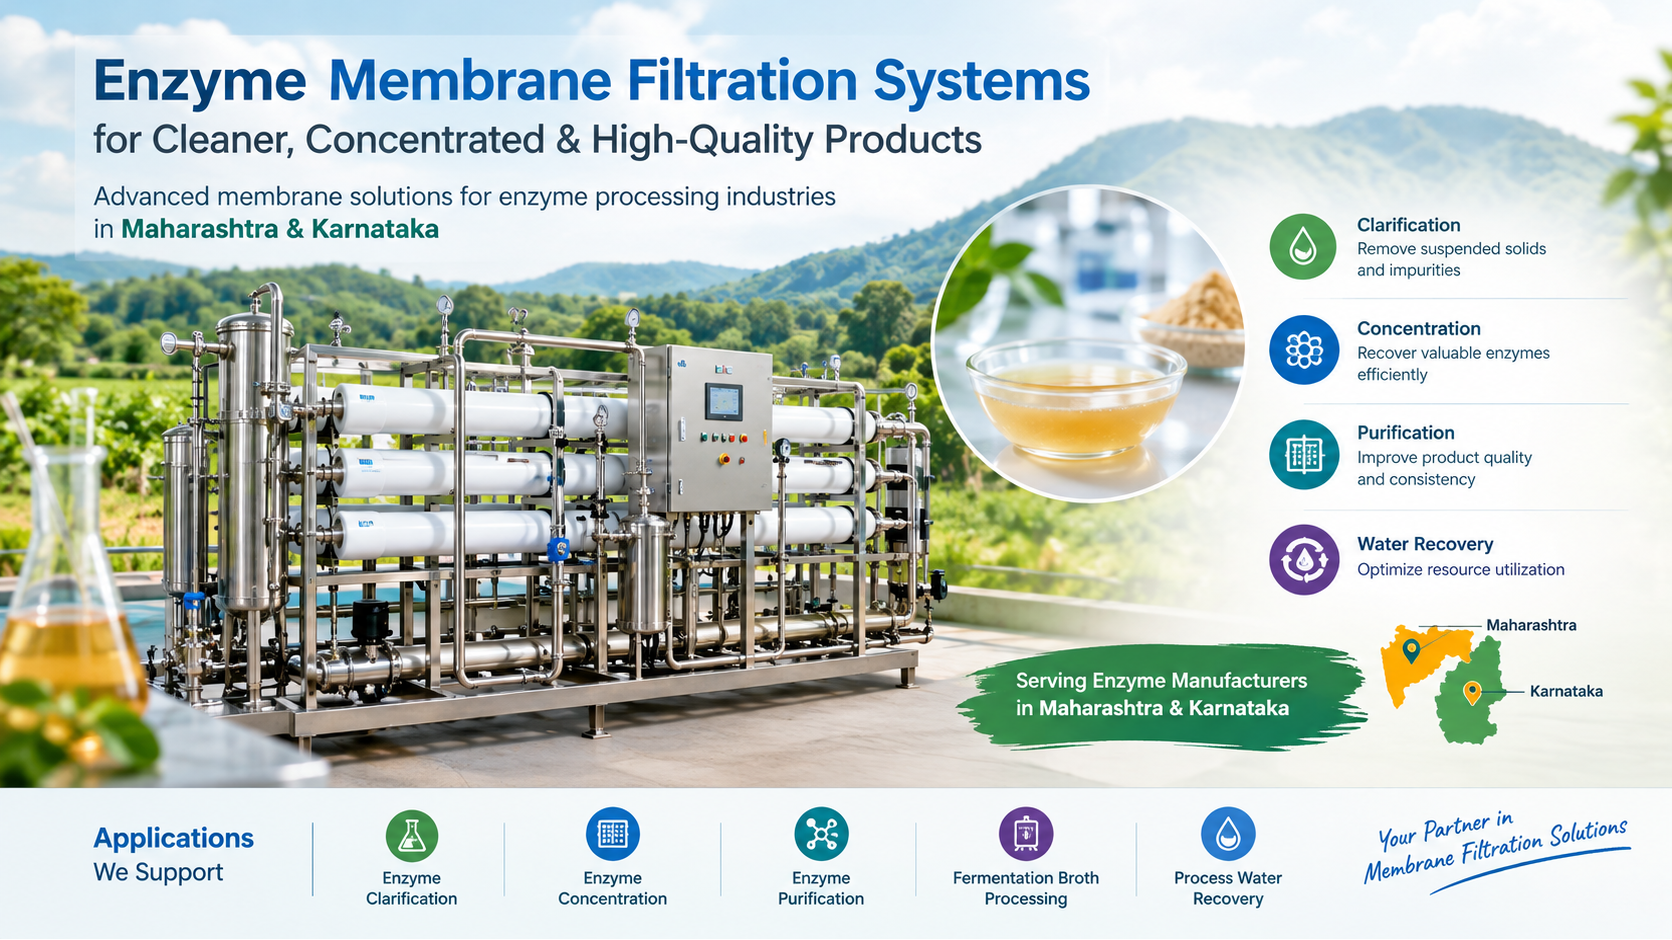
Enzyme Filtration and Purification Systems in Maharashtra and Karnataka, India Advanced Membrane Filtration Solutions for Enzyme Industries The enzyme industry requires efficient separation, clarification, concentration, and purification technologies to produce high-quality enzymes for industrial and commercial applications. Aquaneel Separation Pvt. Ltd. provides advanced membrane filtration systems for enzyme processing industries in Maharashtra and Karnataka, India, helping manufacturers improve product quality, process efficiency, and resource utilization. Membrane filtration technology offers an effective solution for processing enzyme-containing liquids, fermentation broths, and biological process streams. Depending on the enzyme characteristics and process requirements, Microfiltration (MF), Ultrafiltration (UF), Nanofiltration (NF), and Reverse Osmosis (RO) can be used for clarification, enzyme concentration, removal of suspended impurities, and water recovery. Membrane Filtration for Enzyme Manufacturing Enzyme production involves fermentation, extraction, clarification, concentration, and downstream purification. Membrane filtration can support several of these stages while helping manufacturers achieve consistent process performance. Key applications include: Enzyme Clarification: Removal of suspended solids, cells, and other particulate impurities from enzyme solutions and fermentation broths using suitable membrane filtration systems. Enzyme Concentration: Ultrafiltration membranes can concentrate many enzyme proteins while allowing water and selected low-molecular-weight components to pass through. Enzyme Purification: Membrane processes can help separate selected impurities and improve the quality of enzyme preparations, depending on molecular characteristics and operating conditions. Fermentation Broth Processing: Membrane filtration can support the separation of biomass and clarification of fermentation-derived liquids. Process Water Recovery: Suitable membrane systems can help recover reusable water from selected process streams. Product Quality Improvement: Controlled filtration can support consistent product quality and reduce the load on subsequent processing stages. Enzyme Industry Applications in Maharashtra Maharashtra has a diverse industrial base, including biotechnology, pharmaceuticals, food processing, fermentation, and specialty chemical manufacturing. Enzyme manufacturers and biotechnology companies can benefit from membrane filtration systems designed for their specific process requirements. Aquaneel Separation Pvt. Ltd. offers membrane-based process solutions for enzyme concentration, fermentation broth clarification, protein separation, and liquid processing applications in Mumbai, Pune, Nashik, Chhatrapati Sambhajinagar, Kolhapur, and other industrial locations across Maharashtra. Enzyme Filtration Solutions in Karnataka Karnataka is an important centre for biotechnology, life sciences, pharmaceutical manufacturing, food processing, and industrial biotechnology. Membrane filtration technology can support enzyme manufacturers seeking efficient downstream processing and reliable product concentration. Aquaneel Separation Pvt. Ltd. provides application-oriented membrane filtration solutions for enzyme processing industries in Bengaluru, Mysuru, Mangaluru, Hubballi, Belagavi, and other industrial areas across Karnataka. Our systems can be evaluated for enzyme clarification, protein concentration, fermentation liquid processing, and process water recovery, subject to the feed composition and required product specifications. Why Choose Aquaneel Separation Pvt. Ltd.? Aquaneel Separation Pvt. Ltd. specializes in membrane filtration systems for industrial liquid processing and separation applications. Our solutions are developed around process-specific requirements, including: Selection of suitable membrane technology according to the enzyme and feed characteristics. Concentration and clarification of enzyme-containing process streams. Modular system configurations for different production capacities. Process optimization to support product recovery and operational efficiency. Integration with existing production and downstream processing systems. Application-specific trials to evaluate membrane performance and product quality. Choose the Right Membrane Filtration System for Enzymes The selection of a membrane filtration system depends on enzyme molecular weight, feed composition, operating temperature, pH, viscosity, required concentration, and product recovery targets. Membrane selection and operating conditions should also preserve enzyme activity and minimize fouling. Aquaneel Separation Pvt. Ltd. works with enzyme and biotechnology manufacturers in Maharashtra, Karnataka, and across India to evaluate suitable membrane filtration solutions for their processing requirements. Contact Aquaneel Separation Pvt. Ltd. to discuss your enzyme filtration, concentration, or purification application and identify a suitable membrane-based process solution. Website: https://www.aquaneelseperation.in/ Email: projects@aquaneelseperation.in Phone: +91 80002 27156 Aquaneel Separation Pvt. Ltd. – Membrane Filtration Systems for Enzyme Processing in Maharashtra, Karnataka, and India.


This is your website preview.
Currently it only shows your basic business info. Start adding relevant business details such as description, images and products or services to gain your customers attention by using Boost 360 android app / iOS App / web portal.
Enzyme Filtration and Purification Systems in Maharashtra and Karnataka, India Advanced Membrane Fi...
2026-10-10T03:45:02
Enzyme Filtration and Purification Systems in Maharashtra and Karnataka, India Advanced Membrane Filtration Solutions for Enzyme Industries The enzyme industry requires efficient separation, clarification, concentration, and purification technologies to produce high-quality enzymes for industrial and commercial applications. Aquaneel Separation Pvt. Ltd. provides advanced membrane filtration systems for enzyme processing industries in Maharashtra and Karnataka, India, helping manufacturers improve product quality, process efficiency, and resource utilization. Membrane filtration technology offers an effective solution for processing enzyme-containing liquids, fermentation broths, and biological process streams. Depending on the enzyme characteristics and process requirements, Microfiltration (MF), Ultrafiltration (UF), Nanofiltration (NF), and Reverse Osmosis (RO) can be used for clarification, enzyme concentration, removal of suspended impurities, and water recovery. Membrane Filtration for Enzyme Manufacturing Enzyme production involves fermentation, extraction, clarification, concentration, and downstream purification. Membrane filtration can support several of these stages while helping manufacturers achieve consistent process performance. Key applications include: Enzyme Clarification: Removal of suspended solids, cells, and other particulate impurities from enzyme solutions and fermentation broths using suitable membrane filtration systems. Enzyme Concentration: Ultrafiltration membranes can concentrate many enzyme proteins while allowing water and selected low-molecular-weight components to pass through. Enzyme Purification: Membrane processes can help separate selected impurities and improve the quality of enzyme preparations, depending on molecular characteristics and operating conditions. Fermentation Broth Processing: Membrane filtration can support the separation of biomass and clarification of fermentation-derived liquids. Process Water Recovery: Suitable membrane systems can help recover reusable water from selected process streams. Product Quality Improvement: Controlled filtration can support consistent product quality and reduce the load on subsequent processing stages. Enzyme Industry Applications in Maharashtra Maharashtra has a diverse industrial base, including biotechnology, pharmaceuticals, food processing, fermentation, and specialty chemical manufacturing. Enzyme manufacturers and biotechnology companies can benefit from membrane filtration systems designed for their specific process requirements. Aquaneel Separation Pvt. Ltd. offers membrane-based process solutions for enzyme concentration, fermentation broth clarification, protein separation, and liquid processing applications in Mumbai, Pune, Nashik, Chhatrapati Sambhajinagar, Kolhapur, and other industrial locations across Maharashtra. Enzyme Filtration Solutions in Karnataka Karnataka is an important centre for biotechnology, life sciences, pharmaceutical manufacturing, food processing, and industrial biotechnology. Membrane filtration technology can support enzyme manufacturers seeking efficient downstream processing and reliable product concentration. Aquaneel Separation Pvt. Ltd. provides application-oriented membrane filtration solutions for enzyme processing industries in Bengaluru, Mysuru, Mangaluru, Hubballi, Belagavi, and other industrial areas across Karnataka. Our systems can be evaluated for enzyme clarification, protein concentration, fermentation liquid processing, and process water recovery, subject to the feed composition and required product specifications. Why Choose Aquaneel Separation Pvt. Ltd.? Aquaneel Separation Pvt. Ltd. specializes in membrane filtration systems for industrial liquid processing and separation applications. Our solutions are developed around process-specific requirements, including: Selection of suitable membrane technology according to the enzyme and feed characteristics. Concentration and clarification of enzyme-containing process streams. Modular system configurations for different production capacities. Process optimization to support product recovery and operational efficiency. Integration with existing production and downstream processing systems. Application-specific trials to evaluate membrane performance and product quality. Choose the Right Membrane Filtration System for Enzymes The selection of a membrane filtration system depends on enzyme molecular weight, feed composition, operating temperature, pH, viscosity, required concentration, and product recovery targets. Membrane selection and operating conditions should also preserve enzyme activity and minimize fouling. Aquaneel Separation Pvt. Ltd. works with enzyme and biotechnology manufacturers in Maharashtra, Karnataka, and across India to evaluate suitable membrane filtration solutions for their processing requirements. Contact Aquaneel Separation Pvt. Ltd. to discuss your enzyme filtration, concentration, or purification application and identify a suitable membrane-based process solution. Website: https://www.aquaneelseperation.in/ Email: projects@aquaneelseperation.in Phone: +91 80002 27156 Aquaneel Separation Pvt. Ltd. – Membrane Filtration Systems for Enzyme Processing in Maharashtra, Karnataka, and India.
2026-10-10T03:45:02


Submit Your Enquiry